
Engineered carbonization process control, thermal reliability and industrial-
scale manufacturing.

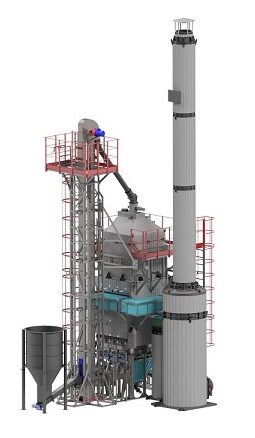

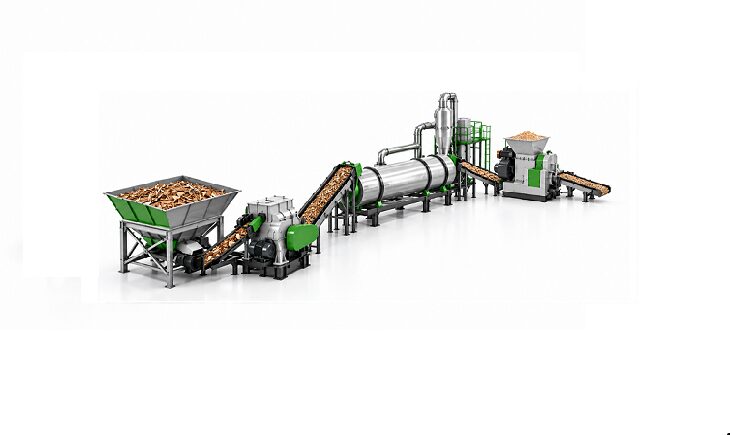

Why Greenpower
Engineering Reliability at Industrial Scale

Process control & thermal engineering
Advanced oxidative reactions of pyrolysis gases management and temperature stabilization ensure eco consistent system performance and operational safety

Industrial-scale carbonization systems
Engineered for continuous bio-carbon production by high-capacity energy efficient conditions

In-house r&d, engineering & manufacturing
Full-cycle integration from design to fabrication guarantees quality control and technical consistency at every stage

Decarbonization
Our systems are designed to reduce emissions and improve energy efficiency in line with modern industrial environmental standards
Choose Your Carbonization Project Type: Certification-Ready Projects or CAPEX-Optimized Projects
Request Consultation by Carbo-boy AI Screening
About GREENPOWER
GreenPower is an international engineering company specializing in industrial biomass pyrolysis and carbonization systems.
We design and manufacture complete thermal processing solutions, including pyrolysis units, raw material drying systems, combustion devices, and automated control systems (ACS) for precise process management.
Our portfolio includes mobile carbonization unit (EKKO-2iq), continuous dry pyrolysis systems (BIO-Carbon), and integrated supporting equipment designed for stable, high-capacity industrial operation.
GreenPower combines in-house engineering, manufacturing, and applied research in biochar and emission reduction technologies. With over 20 years of expertise and internationally protected solutions, we deliver reliable systems aligned with global industrial and environmental standards.
PARTNERSHIP program
Embrace the Power of Clean Energy Investments
GreenPower’s PARTNERSHIP program allows selected partners to establish production of GreenPower carbonization equipment in their regions. Partners receive marketing and manufacturing support, technical documentation and access to selected GreenPower technology packages, including: mobile "EKKO-2iq", modular "Multi-ECO" pyrolysis units and "BIO-Carbon" continuous carbonization systems, depending on the production scales and technical tasks.
Detailed description
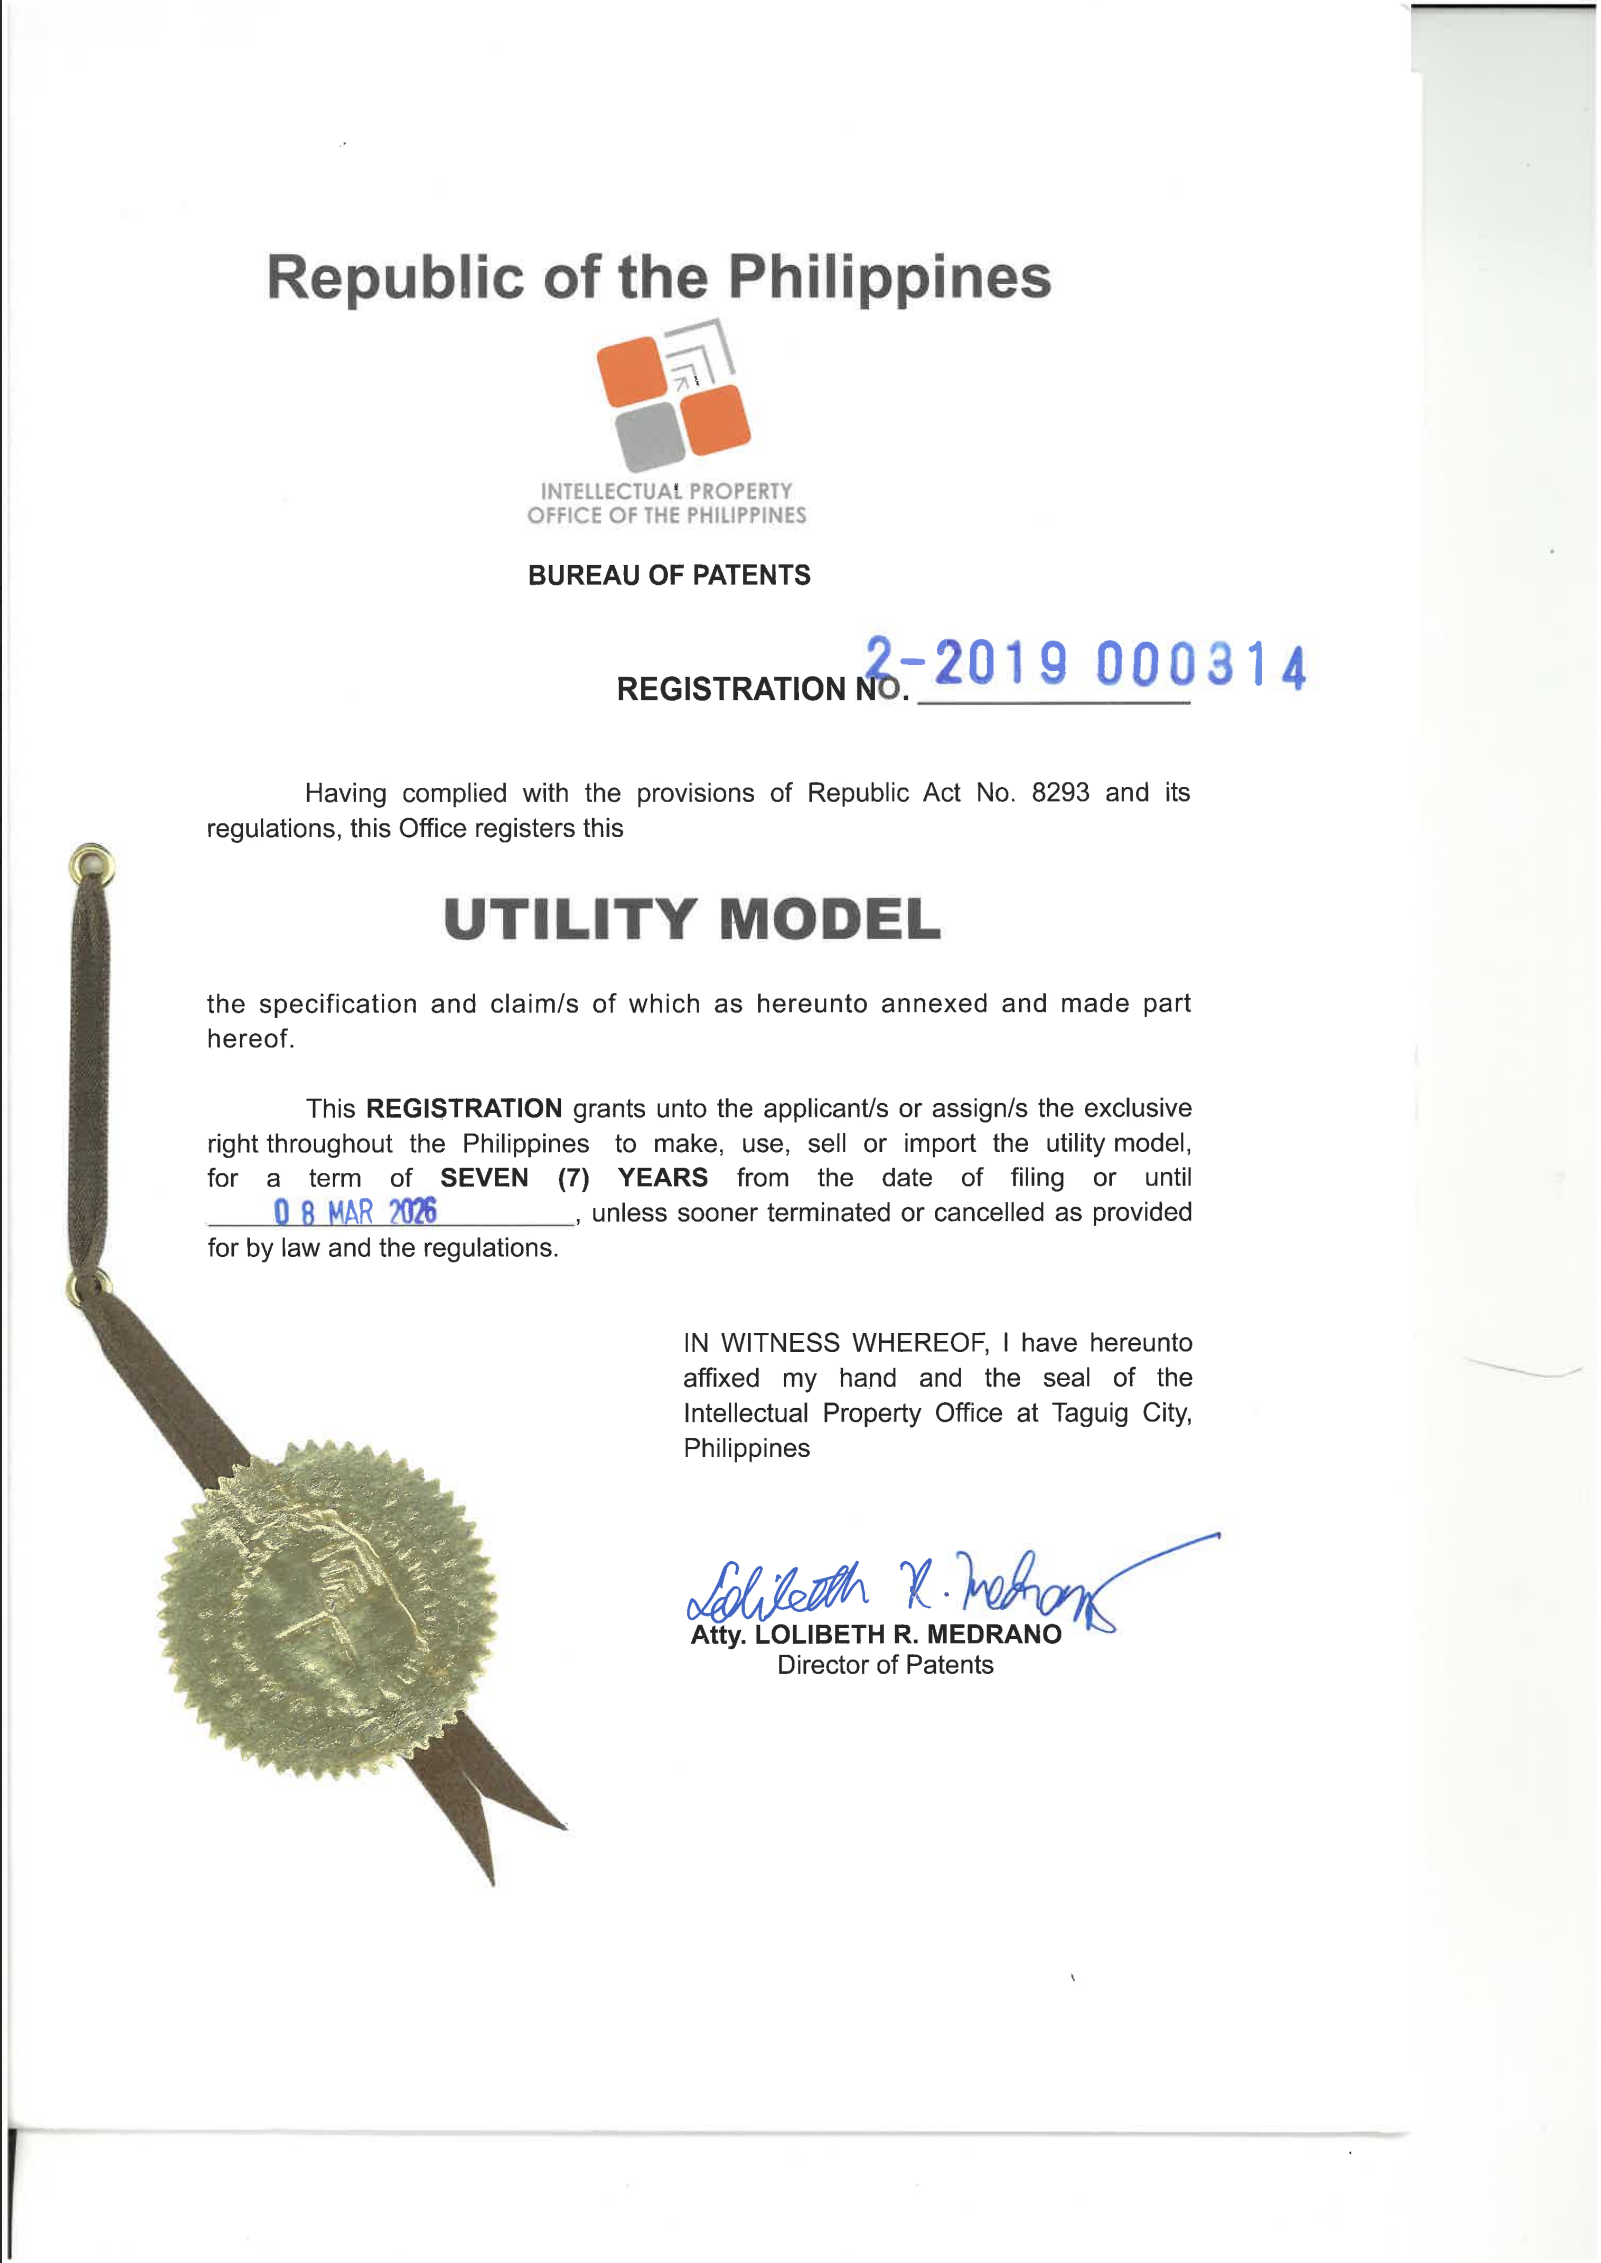
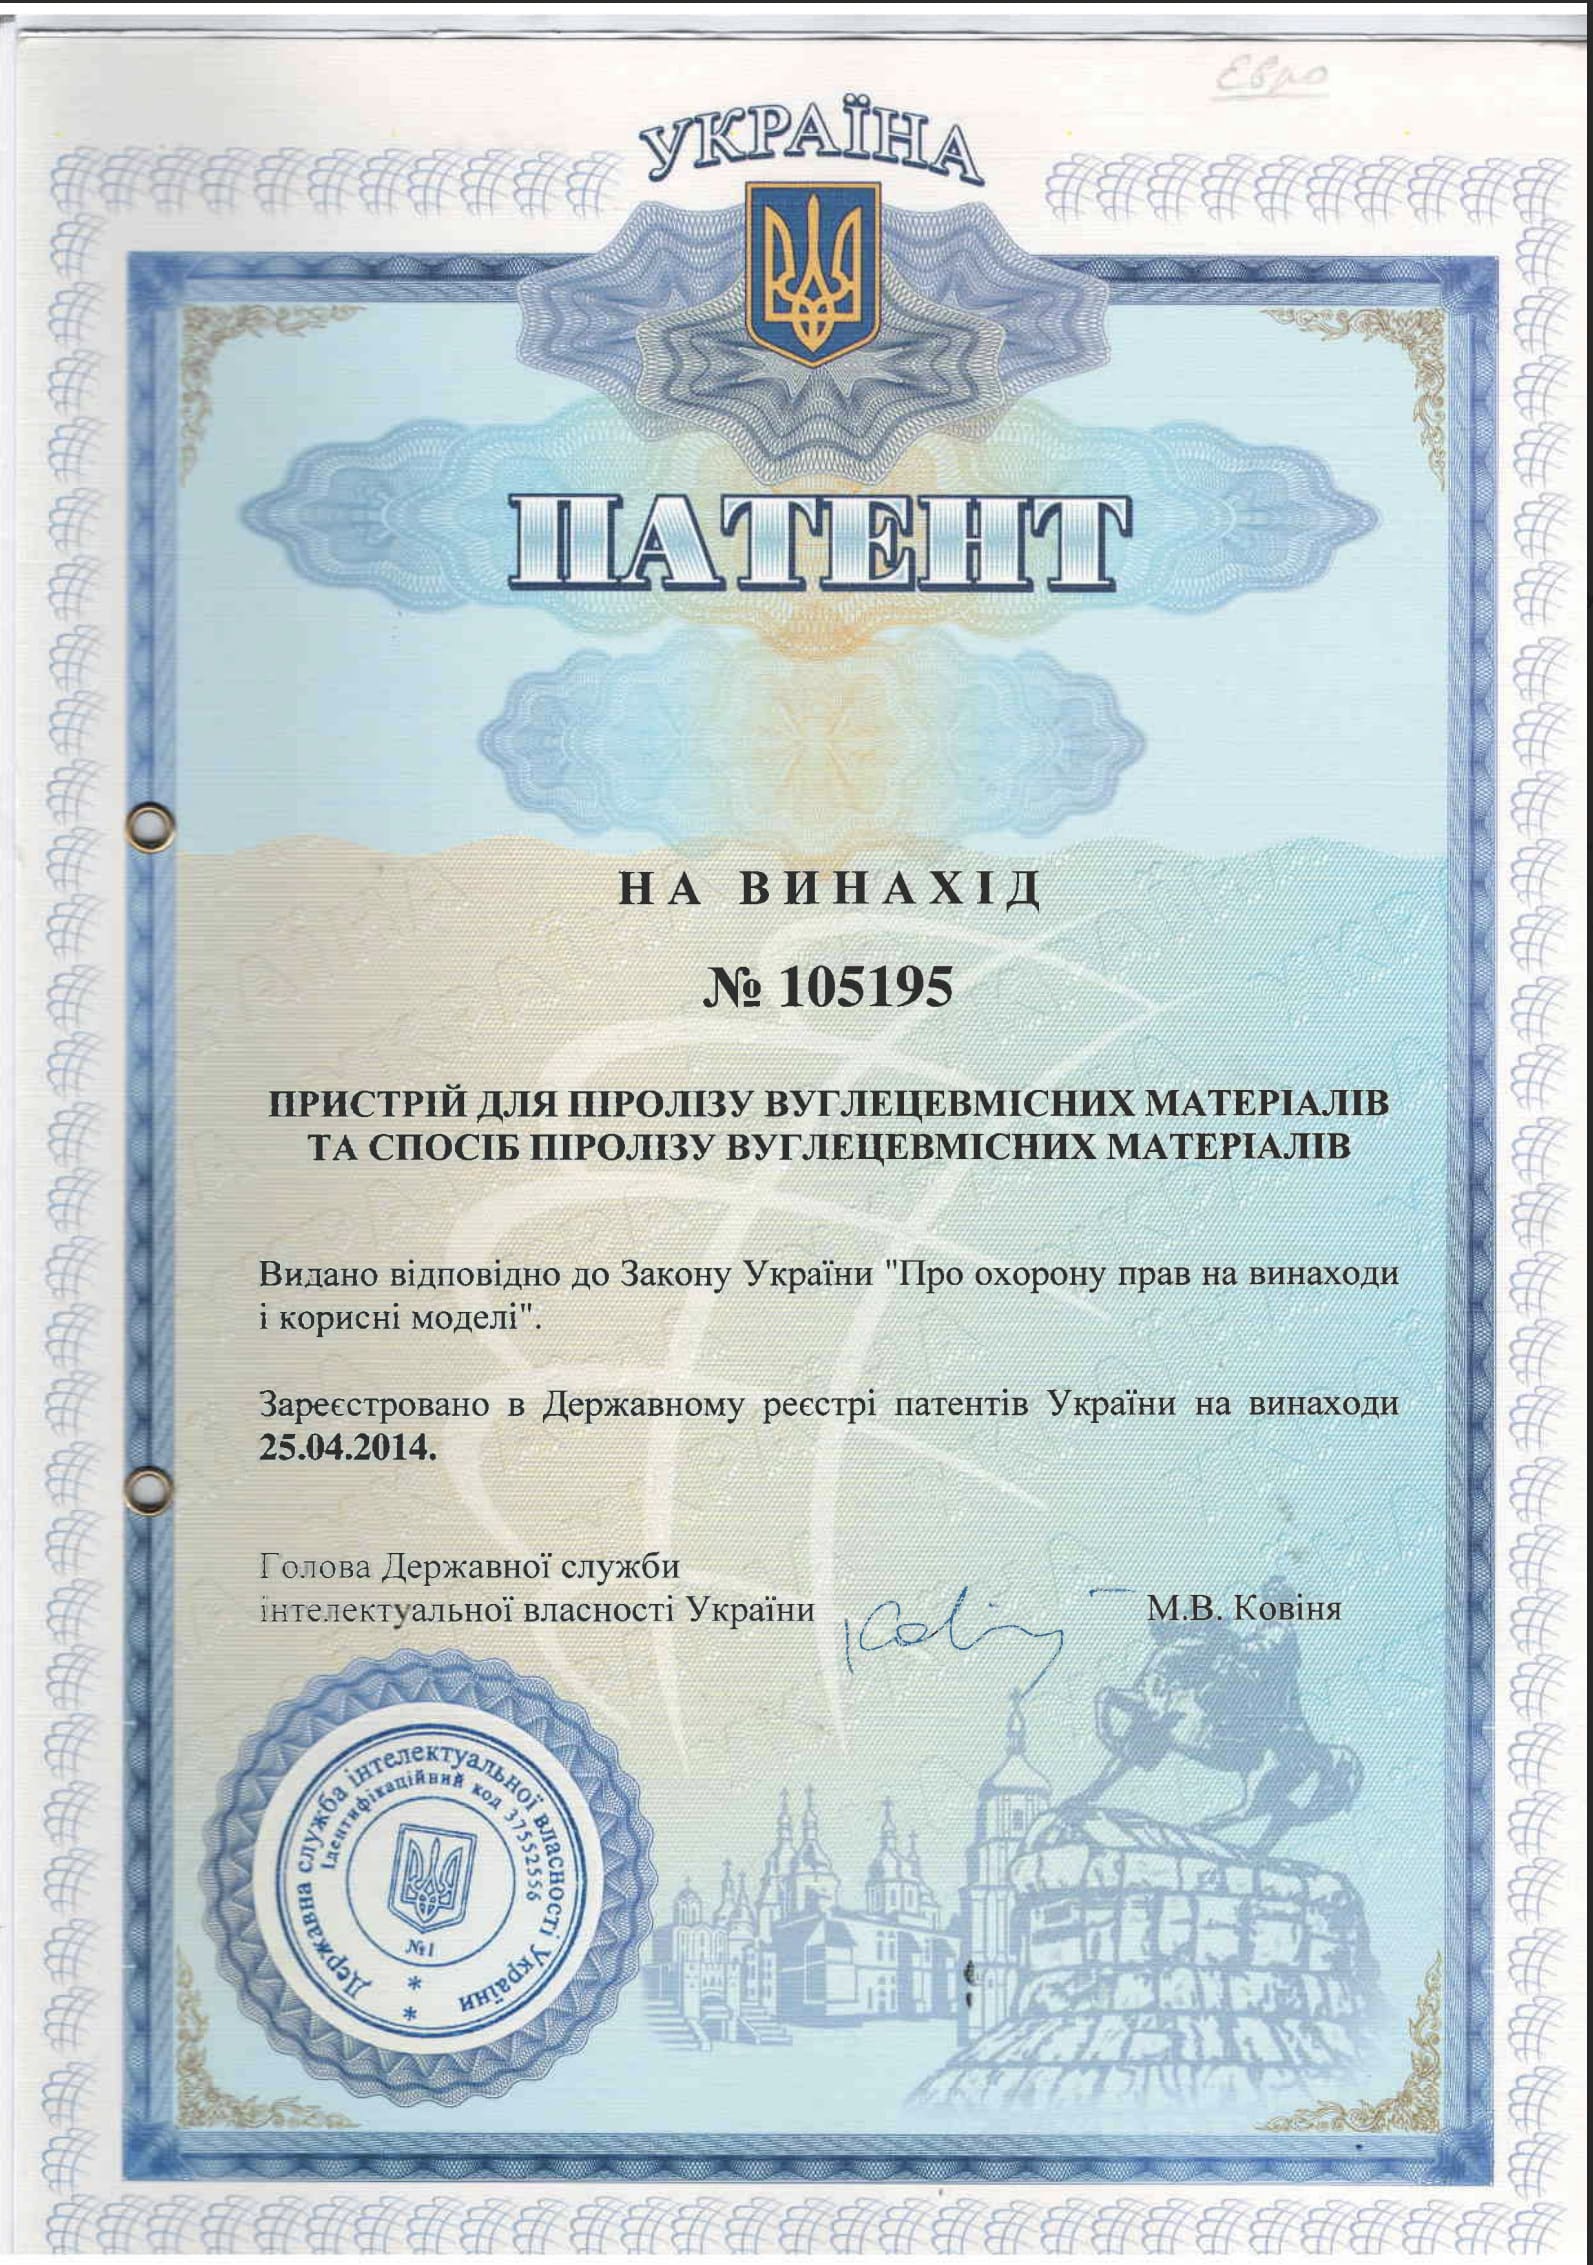
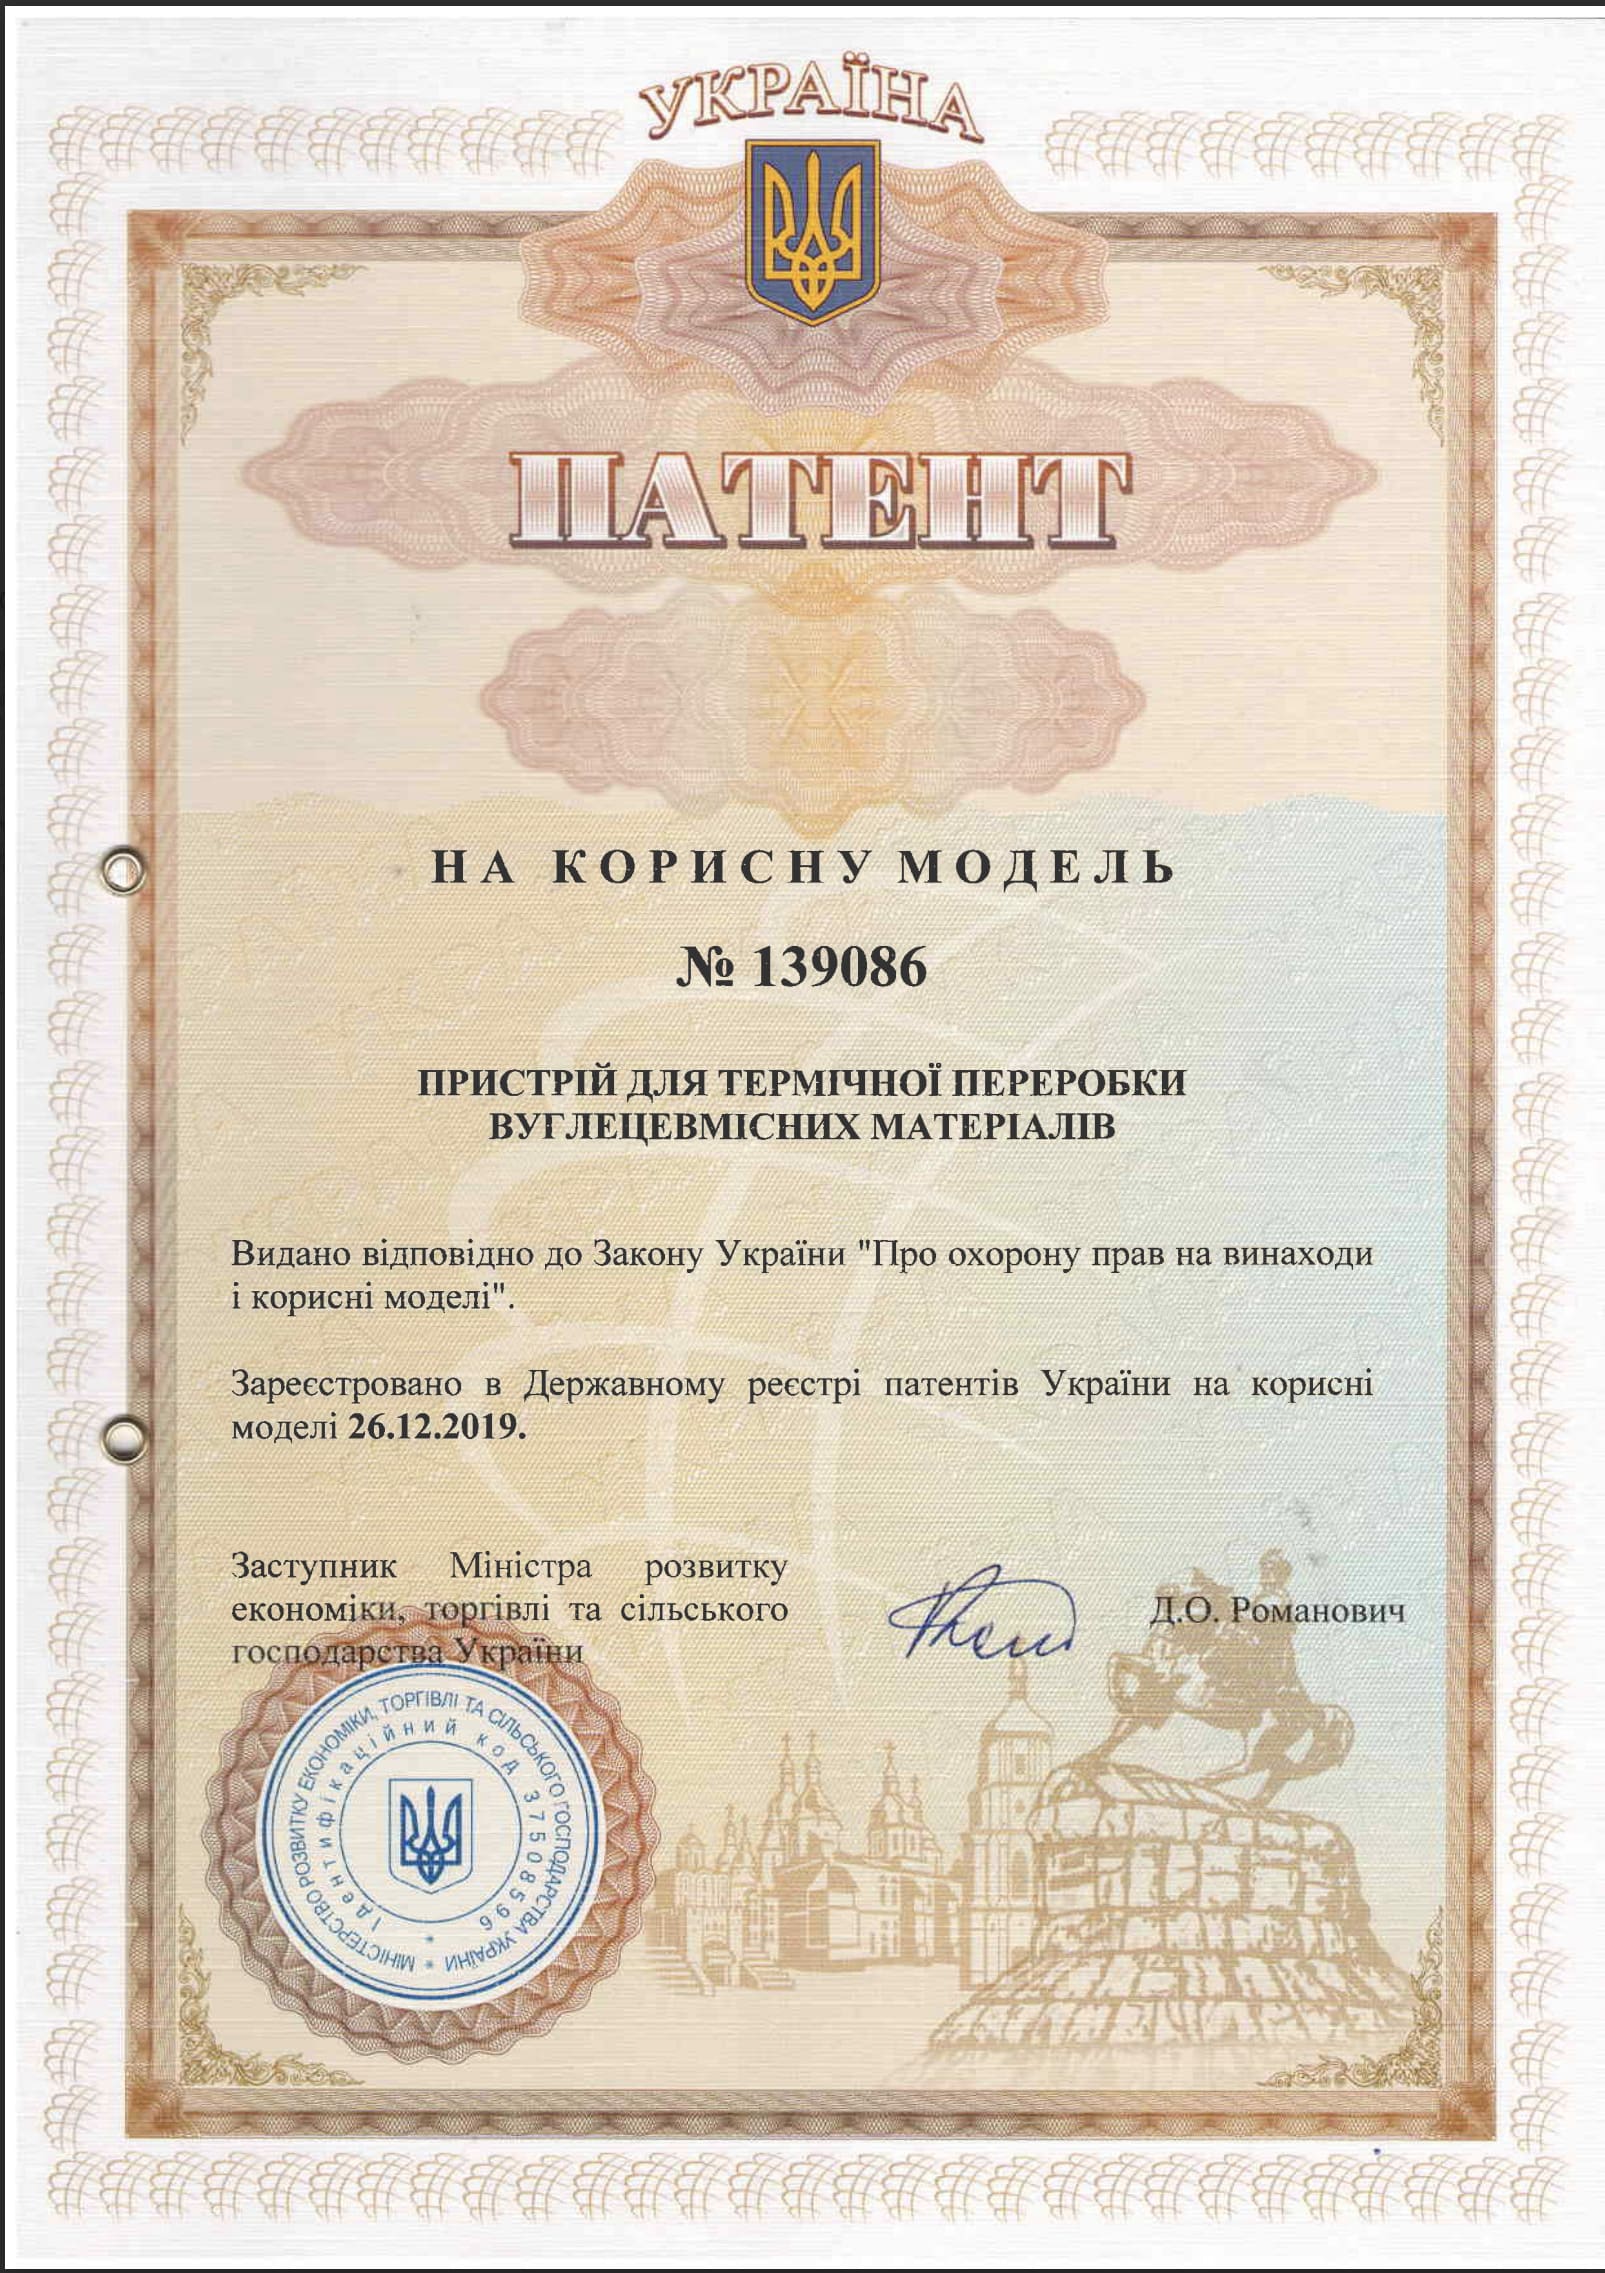
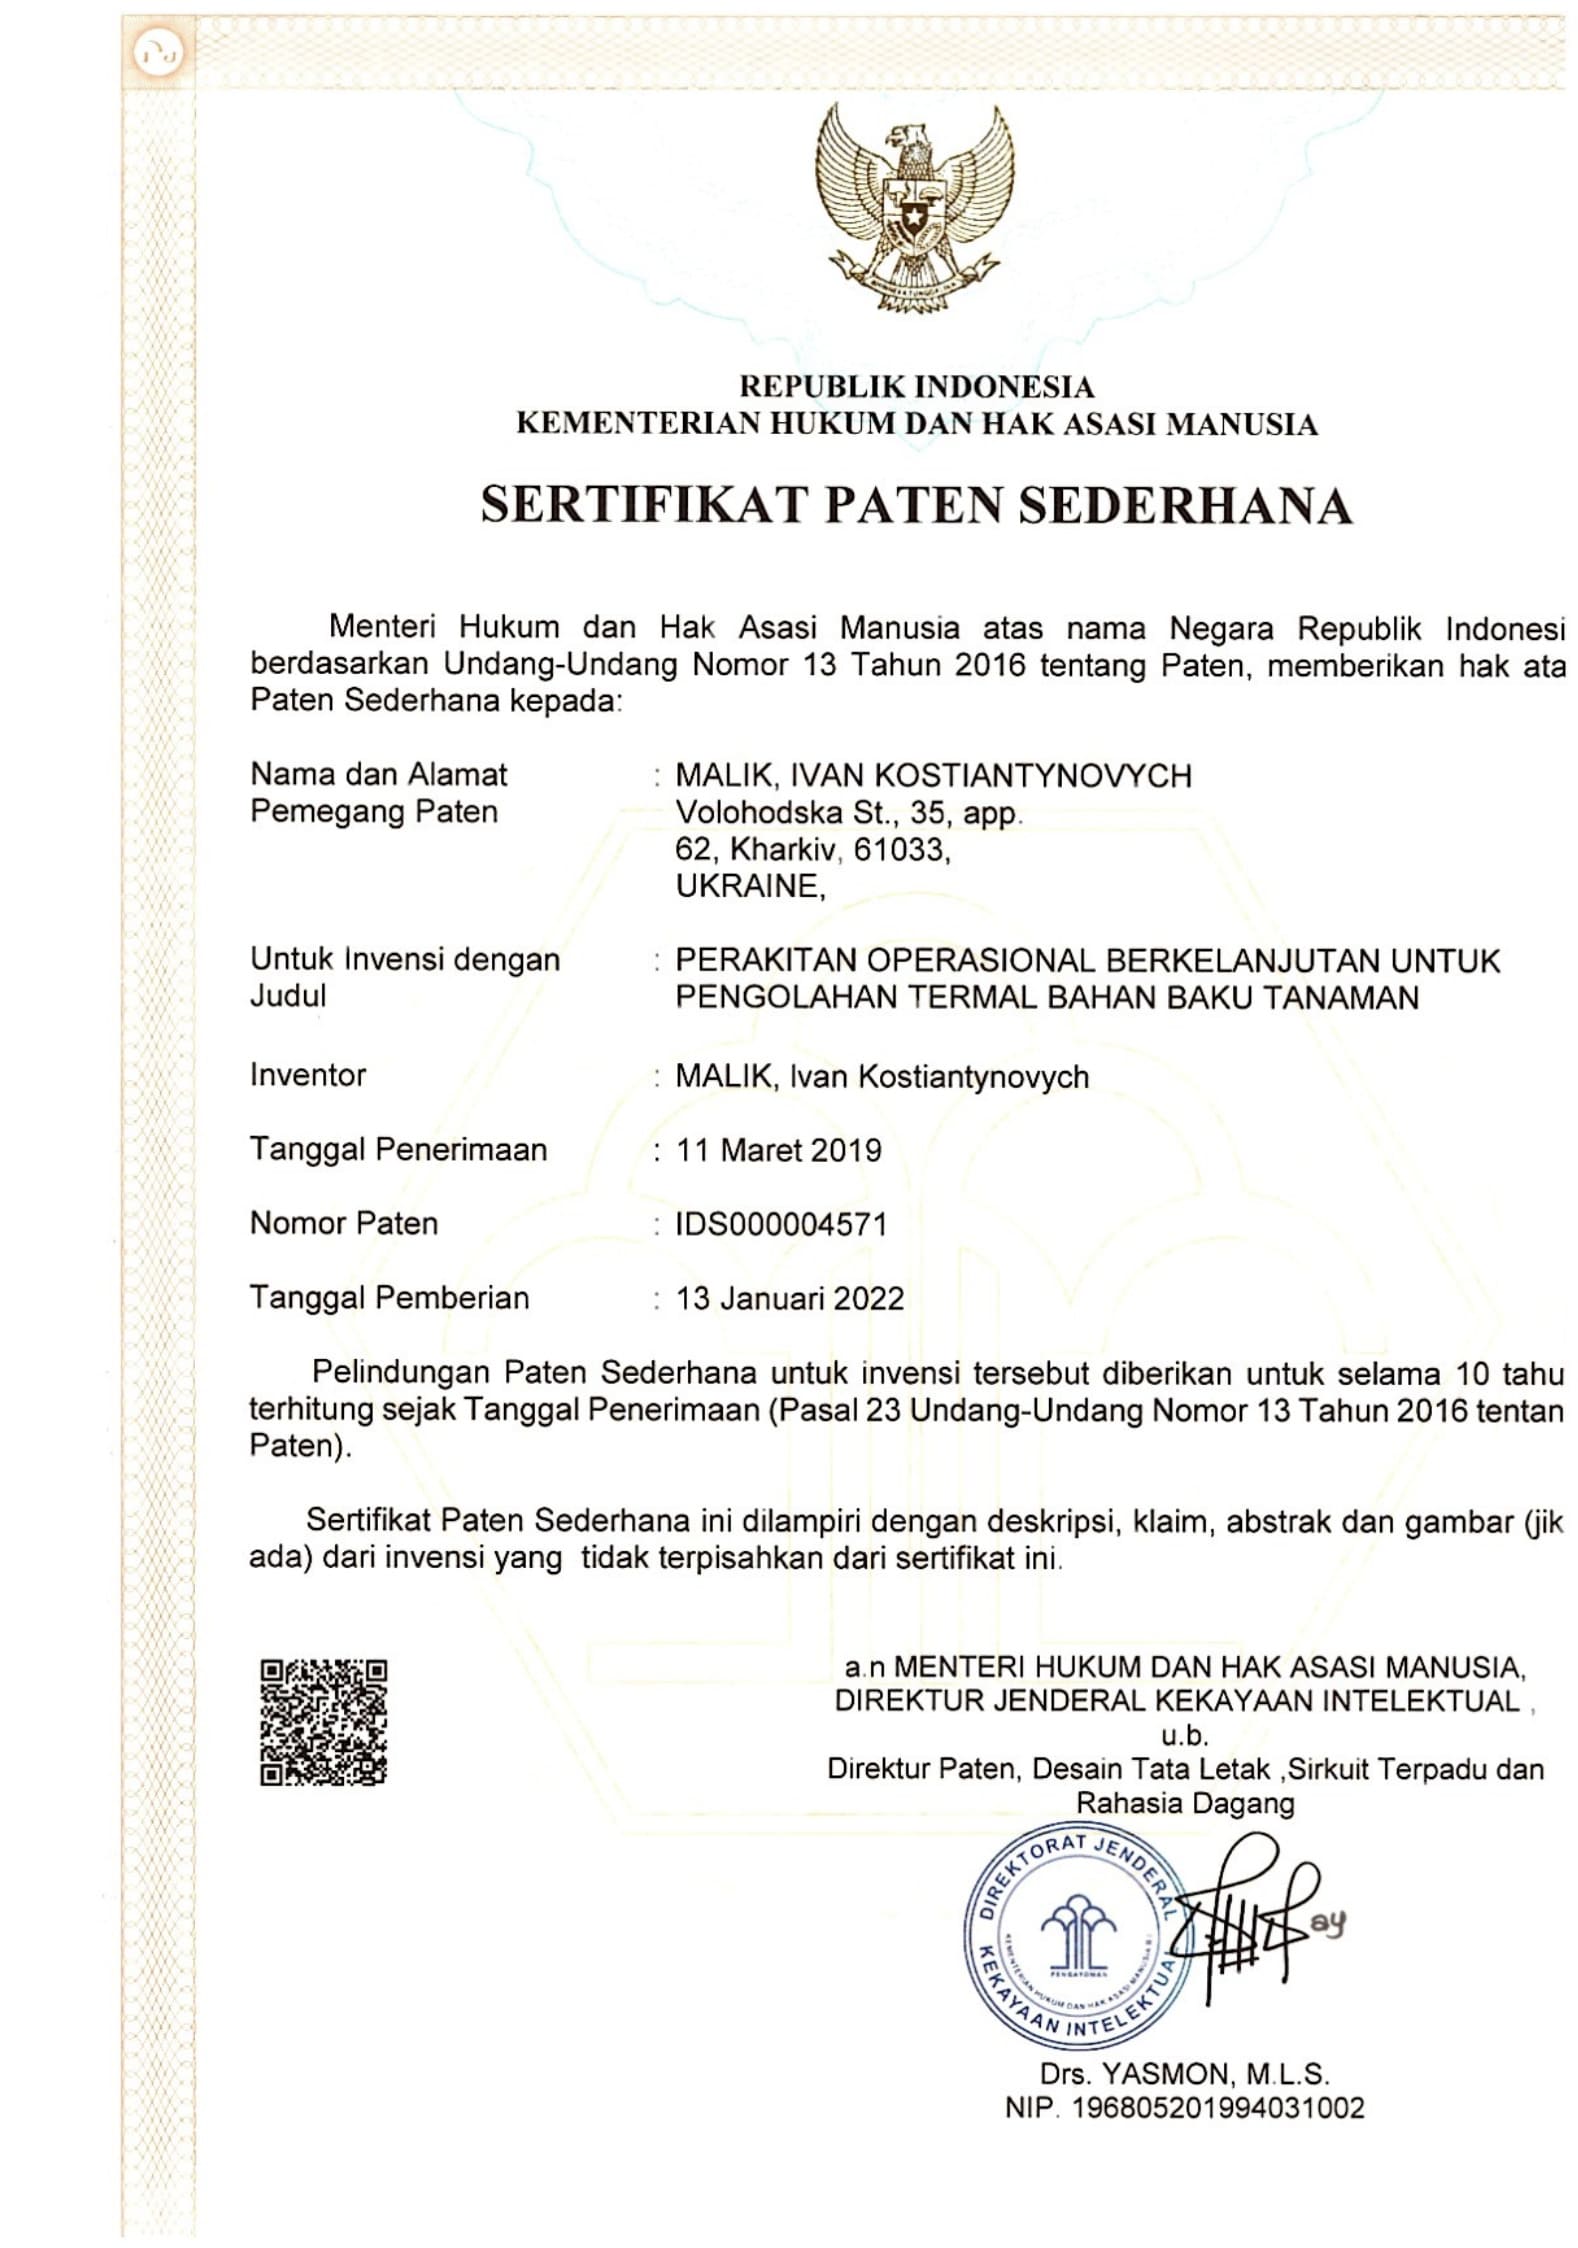
Our certificates
International compliance & industrial standards
Latest news
All News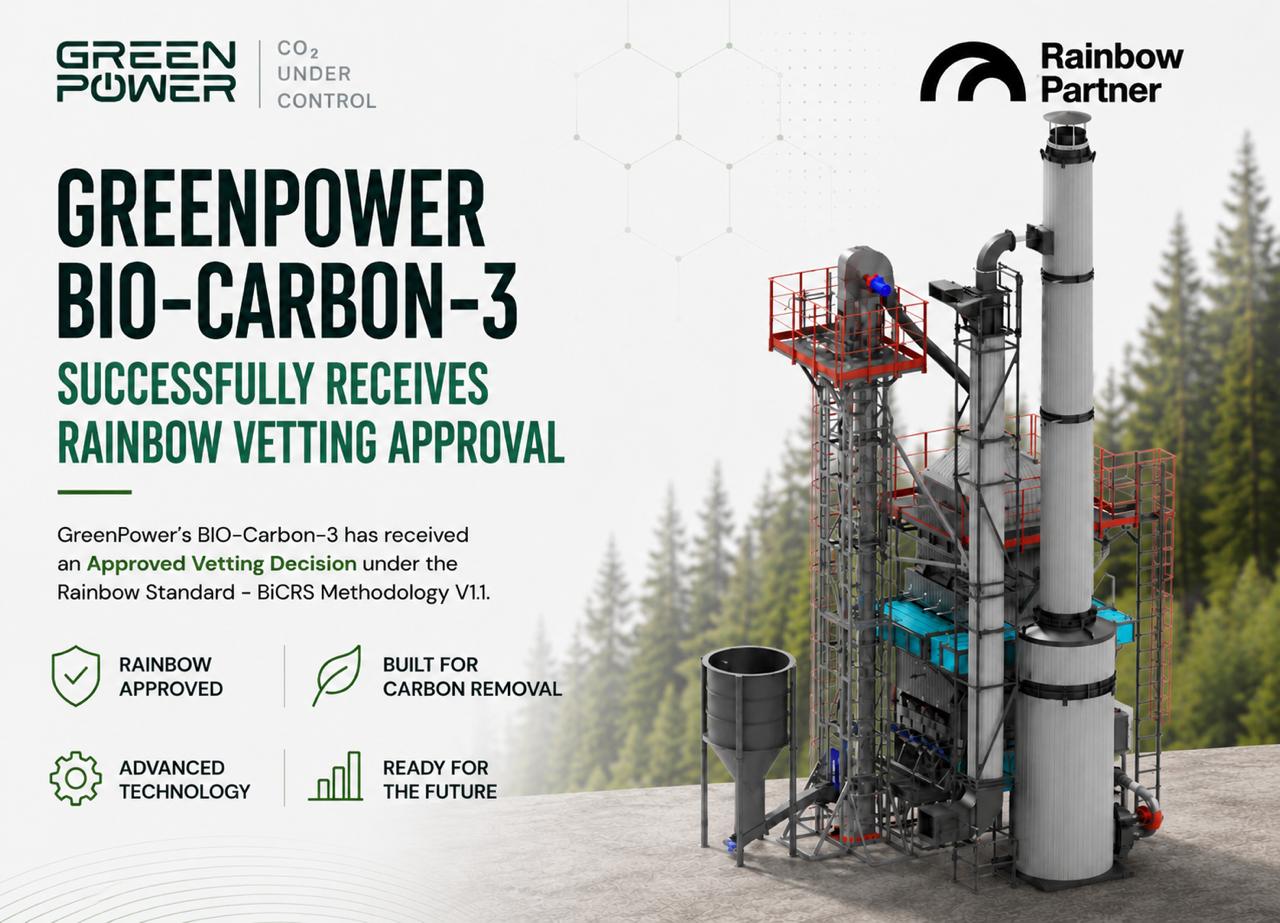
BIO-Carbon-3 Carbonization System Successfully Passes Rainbow Standard Assessment
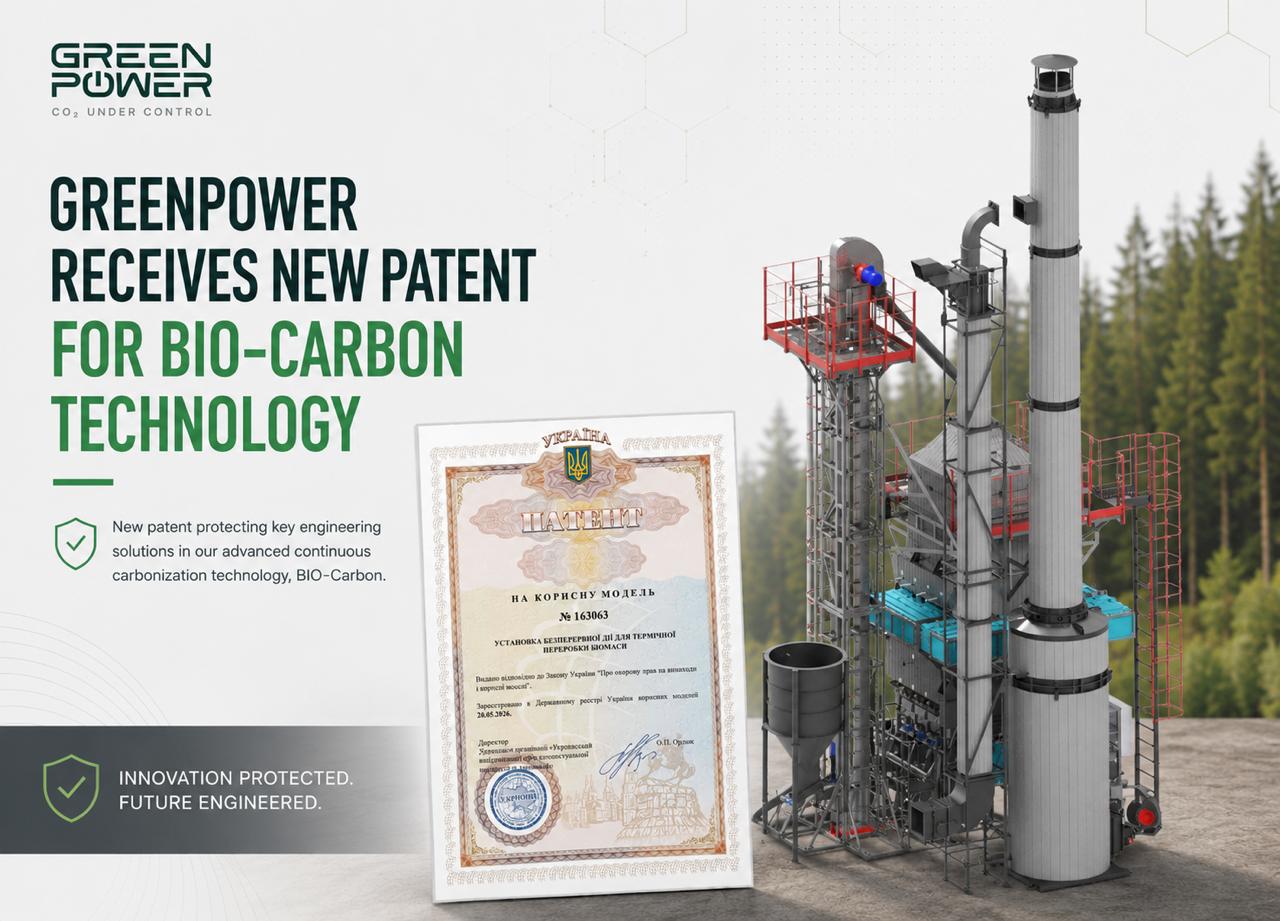
GreenPower Receives a New Patent for BIO-Carbon Technology
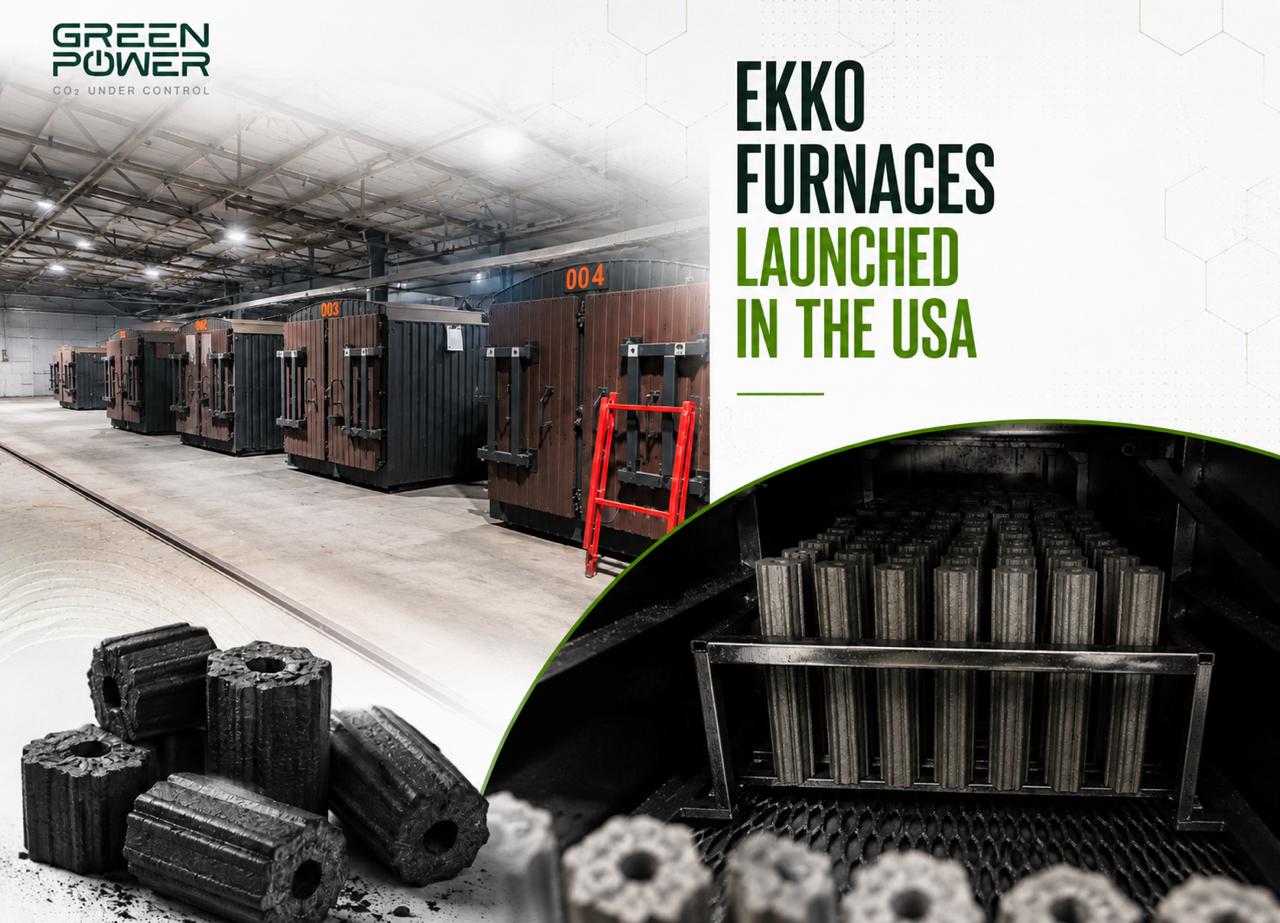
EKKO Carbonization Complex Successfully Launched in the USA

SOLEMN CEREMONY WAS HELD TO CELEBRATE THE OPENING OF A NEW CARBONIZATION SITE IN BHUTAN
Articles
All Articles
FeSi Charcoal Production Concept
Feedstock Preparation and Carbonization Concept for Production of Metallurgical Charcoal for FeSi 1. Mechanical Strength of Metallurgical Charcoal and the Importance of Minimizing Fines For FeSi production, the size of the charcoal fraction is important; however, the key technical parameter is the mechanical strength of the charcoal and its ability to withstand transportation, storage, handling,
BIO-CARBON-3 and EBC requirements: how to ensure controlled combustion of pyrolysis gases
BIO‑CARBON‑3 meets the key engineering requirements of the EBC standard for pyrolysis plants when using pyrolysis gases and control modes: 1) The principle of handling pyrolysis gasesThe BIO-CARBON-3 utilizes a design that prevents pyrolysis gases from being released into the atmosphere without treatment: all steam and gas are directed to a high-temperature, two-stage afterburner. This
Fundamental Technological Approach to the Design of GREENPOWER Pyrolysis Systems
1. “Dry” Pyrolysis Process: Clean and Efficient All GREENPOWER systems are based on dry pyrolysis technology, which eliminates the formation of liquid by-products (such as wood tar and pyrolysis liquids) as production waste. All pyrolysis gases are directed to the combustion chamber and then to the afterburner, generating thermal energy required to sustain the process.
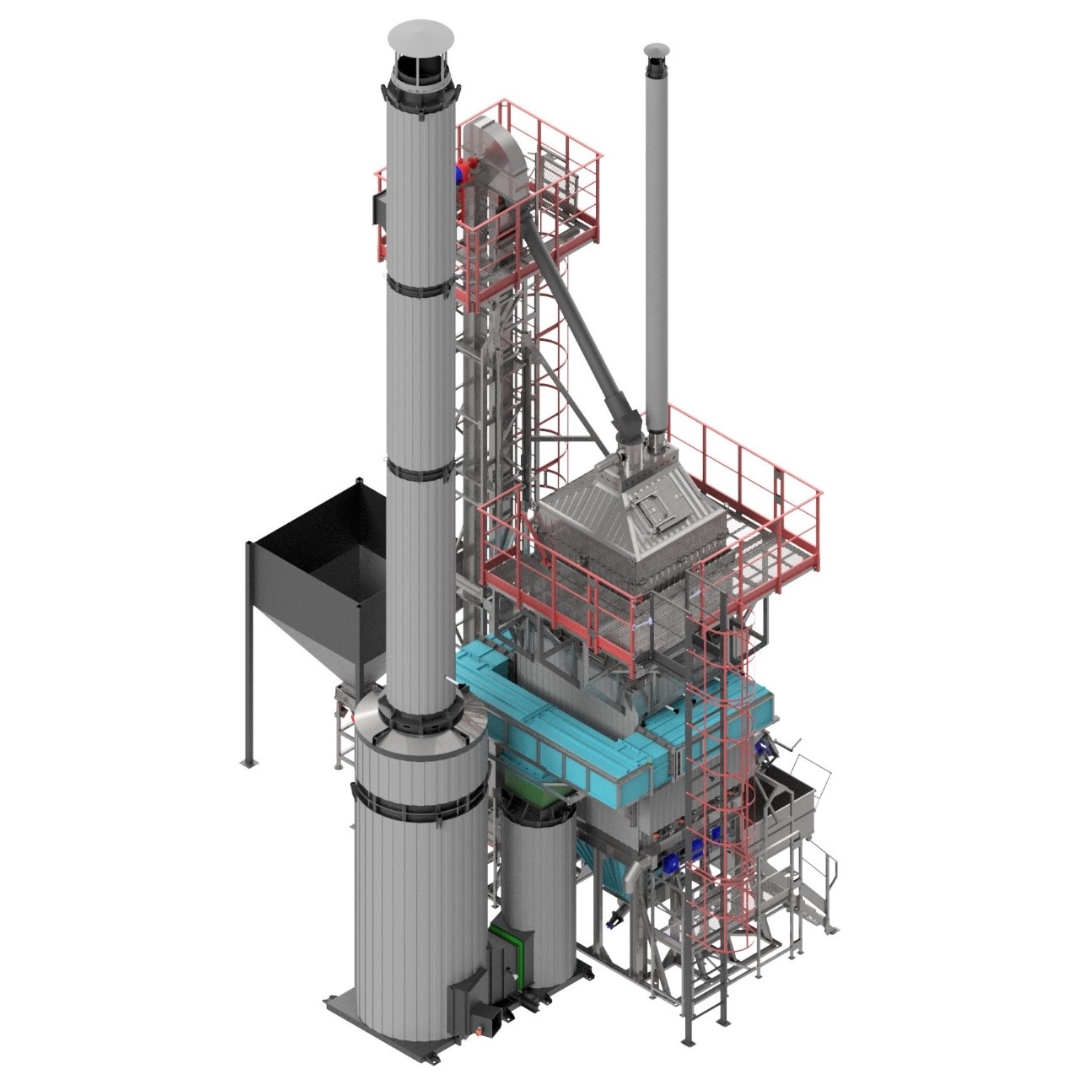
Dry pyrolysis system BIO-CARBON: 24/7 Without Stops, what Economics Look Like Without Cyclical Downtime
In charcoal and biochar production, downtime is often treated as inevitable. Batch systems require cooling, unloading, reheating, and operator intervention between cycles. Each stop reduces effective output, increases labor costs, and creates variability in product quality. Continuous production changes the economic model. BIO-CARBON, developed by GREENPOWER, operates 24/7 without technological stops. The carbonization process is
Faq
Equipment for drying
EKKO-2 Pyrolysis Unit
BIO-CARBON Carbonization Unit
Is the thermal conductivity of wood higher along the fibers or across the fibers?
Along the fibers
How does the density of wood affect thermal conductivity?
The external layers of wood dry much faster than the internal ones. When thick and damp logs are quickly dried, the external layers are dry, while the internal layer are just beginning to lose moisture.
As a result, the drying of wood is uneven. This causes the formation of cracks in it, extending from the
external surface inward along the radius. Cracks in wood are also formed due to faster drying of the heartwood compared to sapwood.
What causes cracks in wood during drying?
Due to intensive moisture removal from wood. To avoid the formation of cracks, it is necessary to lower the temperature of the heat carrier for drying and increase the drying time.
How does the system for extracting excess heat from BIO-KILN work?
Excess heat is taken directly from the chimney after the afterburner. The temperature in the chimney can reach 800-1200°C, atmospheric air is used to lower the temperature. That is, the heat is diluted with cold air, as a result of which the temperature of the heat carrier drops to the required one. This process occurs automatically, the operator only sets the required temperature.
The generated heat carrier can be used for chamber dryer, drum dryer or shaft dryer.
How does the pre-drying system for carbonization furnaces EKKO work?
Excess heat is taken directly from the chimney after the afterburner. At the same time, the better the wood was dried, the more excess heat will be for pre-drying, that is, the drying will be more efficient. We recommend first drying the wood in a pre-dryer, and then loading it into the carbonization chamber when starting work on the kiln. It should be noted that the temperature in the chimney can reach 200-1200°C, atmospheric air is used to lower the temperature. That is, the heat is diluted with cold air, as a result of which the temperature of the heat carrier drops to the required one. This process occurs automatically, the operator only sets the required temperature.
The generated heat carrier can be used for chamber dryer or direct drying in trolleys. Chamber dryer significantly increases the efficiency of wood drying, in comparison with trolleys.
Who are the main consumers (Unit buyers) of EKKO-2?
- Logging and woodworking enterprises (with their own feedstock or waste products).
- Producers of fuel wood and energy crops (eucalyptus, bamboo, energy willow, etc.).
- Agricultural enterprises, orchards, and agro-biomass processors (subject to feedstock preparation and applicability for chamber carbonization).
- Companies generating plant-based biomass/carbon-containing feedstock (including some lump waste).
- Investors/operators of BIOCHAR projects (carbon removal projects, soil improvement, ESG) requiring stable quality and process parameter traceability.
Who are the main consumers of the finished product (charcoal / biochar)?
- BBQ/HoReCa and retail market.
- Metallurgy.
- Silicon production.
- Activated carbon production.
- BIOCHAR as a soil conditioner/eco-friendly fertilizer (depending on application standards).
- Other industries requiring carbon materials (sorbents, filtration, etc. — based on the customer’s technical specifications).
What is EKKO-2 and what is its operating principle?
EKKO-2 is a semi-continuous chamber carbonization (slow pyrolysis) unit equipped with two technological chambers. The process is based on controlled heat supply and the complete neutralization of pyrolysis gases. The thermal energy generated during the neutralization of pyrolysis gases is used for drying the feedstock and maintaining the pyrolysis process, which reduces the need for additional fuel once a stable operating mode is reached.
The main purpose of the EKKO-2 fixed-bed pyrolysis unit is the production of lump charcoal with a minimal content of fine fractions.
What processes take place “outside the Unit” and “inside the Unit”?
A. Processes outside the pyrolysis Unit:
- Feedstock size reduction: cutting and splitting, and in some cases crushing and chopping, i.e. reducing the material to an acceptable fraction, which facilitates thermal processes and loading of feedstock into the trolleys;
- Loading feedstock into the trolleys;
- Pre-drying of feedstock: forced drying using excess heat from the EKKO-2 process;
- Charging the trolley into the chamber and removing the trolley with hot charcoal from the chamber;
- Cooling the charcoal in the trolleys without oxygen access;
- Discharging charcoal from the trolley, and if required, charcoal stabilization and packaging.
B. Processes inside the pyrolysis Unit:
- Final drying and initial stage of pyrolysis (100–250°C): removal of moisture and primary pyrolysis products;
- Carbonization (250–450°C);
- Calcination (approximately 450–550°C): applied when higher fixed carbon content is required (Cfix > 83%).
*Transitions between modes occur according to the ACS algorithms and/or by the operator’s decision;
What operating modes of the chambers are provided?
Pre-drying mode: control of the maximum allowable drying temperature of the feedstock, preventing the onset of pyrolysis reactions in the material;
Typical pyrolysis chamber modes: “DRYING”, “PYROLYSIS START”, “PYROLYSIS END”, “CHARCOAL READY”, “RELOADING”.
What is BIO-CARBON and what is its purpose?General Questions about BIO-CARBON
BIO-CARBON is a vertical moving-bed unit for continuous dry carbonization of biomass. Based on patented technology and full automation, the unit is an industrial asset that produces:
• High-quality charcoal with fixed carbon content (Cfix) from 82% to 95%
• Biochar for agricultural applications
• Industrial charcoal for metallurgy, activated carbon production, semiconductors, and silicon production
• High-potential thermal energy as a by-product
The unit operates 24/7 without technological shutdowns and ensures environmentally friendly production through full neutralization of pyrolysis syngas.
What are the advantages of BIO-CARBON compared to traditional charcoal production methods?
The main advantages of BIO-CARBON include:
- Environmental friendliness: Emissions to the atmosphere consist only of water vapor and CO₂. Pyrolysis gases are fully neutralized at temperatures above 1300°C, eliminating harmful emissions. Compared to traditional methods, which produce up to 4 tons of harmful emissions per 1 ton of charcoal.
- 100% automation: Minimal personnel involvement (1 operator + 1 assistant per shift). Automatic control of all parameters via the 2026 control system.
- Continuous operation: 365 days a year, 24 hours a day, 7 days a week without technological shutdowns.
- Stable product quality: The automated control system ensures consistent characteristics of the produced charcoal.
- Energy efficiency: The unit operates on its own pyrolysis gas; additional fuel is only required during startup (25–50 liters of propane-butane gas). Generates excess heat of 300–1000 kW.
- Low power consumption: BC-2: 8 kW; BC-3: 13.6 kW.
- Compactness: Small footprint with high productivity.
- High reliability: 100% refractory materials, service life of 5–10 years.
What BIO-CARBON models are available?
There are two main unit models, differing in capacity and dimensions:
| Model | Productivity (t/month) | Productivity (t/year) | Energy consumption (kW/h) |
| BIO-CARBON-2 (BС-2) | 40-70* | 440-770 | 8 |
| BIO-CARBON-3 (BС-3) | 80-120* | 880-1320 | 13.6 |
*Note: productivity is specified for a fixed carbon content (Cfix) 82-95%
In which countries are BIO-CARBON unit units used?
GreenPower unit is officially operated in more than 39 countries worldwide, including countries in Europe, Asia, Africa, South America, and North America. The unit has obtained environmental operating permits in all of these regions.
What factors affect the unit’s productivity?
The productivity of BIO-CARBON depends on the following key factors:
- unit model: BIO-CARBON-2: 60–100 t/month; BIO-CARBON-3: 80–140 t/month
- Fixed carbon content (Cfix) in the final product: The lower the required Cfix, the higher the productivity. For example, for the BIO-CARBON model:
- At Cfix 80–85%: up to 120–140 t/month
- At Cfix 90–95%: up to 80 t/month
- Bulk density of the feedstock: Depends on the material density and its particle size. As bulk density increases, the unit productivity increases.
- Feedstock moisture content: Should be below 15% (maximum 20%). Lower moisture increases productivity, while higher moisture decreases it. Optimal moisture: 10–12%.

Discuss Your Carbonization Project
Our engineering team will review your requirements and propose the appropriate system.